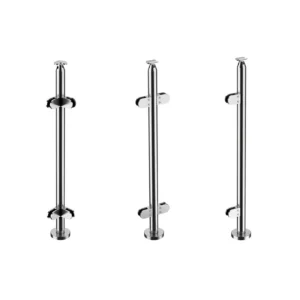
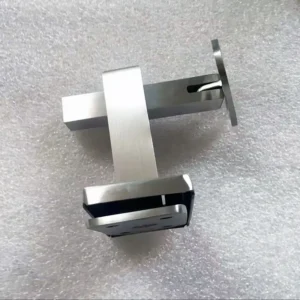
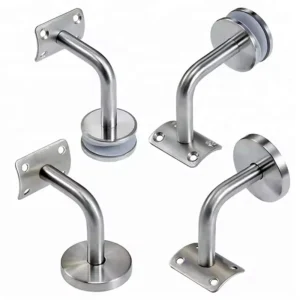
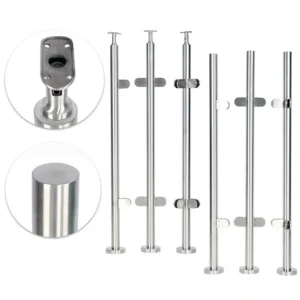
Before releasing an OEM/ODM purchase order for custom stainless steel railing anchors, the buyer has to decide whether the specification package actually describes a producible, inspectable part — or whether it still depends on assumptions that will surface as disputes after production starts. That decision determines whether a prototype round catches problems early or whether a repeat batch inherits them.
What makes a custom anchor specification production-ready
| Specification area | What must be controlled before release | Evidence or boundary to retain |
|---|---|---|
| Drawing and interfaces | Connection interfaces, critical dimensions, threads, tolerances, and mating parts | A controlled released drawing |
| Stainless material | Applicable product form and required material evidence | A broad 304 or 316 label alone is insufficient |
| Finish and passivation | Finish and passivation scope | Grade, treatment, and acceptance criteria remain application-specific and subject to purchaser-supplier agreement |
| Inspection and traceability | Lot traceability, inspection method, and acceptance record | An inspection-document type alone does not prove authenticity, traceability, test validity, or conformity |
| Protective packaging | Packaging appropriate to the anchor’s service environment | The packaging requirement remains project-specific |
| Revision control | Prototype or first-article changes reflected in the released drawing and purchase documents before repeat production | The repeat order must use the released revision basis |
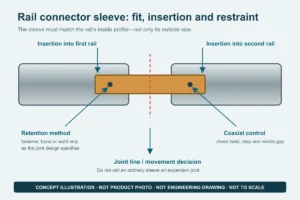
A specification is production-ready when it removes the need for anyone on the shop floor or in incoming inspection to interpret intent. For a railing anchor, that means every connection interface, critical dimension, thread, tolerance, and mating part is fixed on a document both sides have agreed to, rather than implied by a reference sample or a verbal description. Where the anchor must mate with a post, base plate, or structural substrate supplied by another party, the interface geometry has to be defined on both sides of that joint, not just on the anchor itself.
The condition that changes this judgment is how many parties touch the interface before final assembly. Where the anchor is a single self-contained part going into a fabricator’s own post, the drawing only needs to control the anchor’s own features. Where the anchor must coordinate with base plates, fasteners, or structural steel sourced separately — for example where an adjustable base plate is specified from a different line item — the specification has to carry enough shared dimensional data that the two components will actually mate without field rework. A buyer who treats the anchor drawing as complete in isolation, without checking it against the mating part’s drawing, is deferring a coordination problem to the installation stage rather than resolving it at order release.
Material evidence follows the same logic. A callout of a stainless designation without the applicable product form and the evidence required to confirm it leaves open what the supplier will actually deliver. Finish and passivation scope depend on where the anchor will sit in service, and that scope has to be written down, not left to the supplier’s default practice. Traceability and inspection records only have value if the acceptance method is agreed before parts are made, since a record produced after the fact cannot establish what was actually checked against. Packaging has to reflect the anchor’s service environment and shipping path, because protection appropriate for an indoor fit-out is not necessarily sufficient for a component that will sit in transit or storage before an outdoor installation. Revision control closes the loop: whatever changes during prototyping has to be folded back into the released drawing and the purchase documents before a repeat order is placed, or the repeat batch will be built against an outdated basis.
Controlled drawings, interfaces, and dimensional tolerances
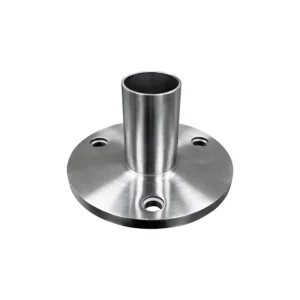
The controlled drawing is the single reference both buyer and manufacturer use to settle disagreements about what was ordered. Its value comes from completeness at the interface, not from general detail across the whole part. For a railing anchor, the interfaces that matter most are the points where the anchor contacts another component: a post base, a structural substrate, a cover plate, or a fastener. Each of these interfaces carries its own critical dimensions — hole patterns, thread engagement, seating faces, clearance for adjustment — and each needs an explicit tolerance rather than an assumed one.
Tolerance choices change with the mating condition. Where an anchor connects to a fixed, non-adjustable base plate, the tolerance on the mounting pattern has to be tight enough that the parts align without additional machining on site. Where the anchor is paired with an adjustable base plate, some of that positional burden shifts to the adjustment mechanism itself, and the anchor’s own tolerance can be set against a different reference point. This is a design decision, not a formality — specifying a tight tolerance where an adjustable interface already compensates for variation adds cost without adding function, while specifying a loose tolerance where no adjustment exists invites a fit problem at installation.
Thread specification deserves the same discipline as linear dimensions. A thread callout needs its form, class, and engagement length defined, along with whether the mating thread is supplied by the anchor manufacturer or by another party in the assembly. Where the anchor threads into a substrate prepared by a different trade — poured concrete, structural steel, or a glass-adjacent frame — the drawing should state which party is responsible for the tolerance on that substrate’s prepared feature, because a dimensionally correct anchor cannot compensate for an out-of-tolerance mating hole.
Mating-part callouts belong on the drawing even when the mating part itself is not part of this purchase order. Listing the mating part’s reference dimensions prevents the anchor from being optimized in isolation and then found incompatible once it reaches final assembly.
Material, thread, finish, and passivation requirements
| 参考文献 | Applicable subject | What the reference can support | What still requires verification or agreement |
|---|---|---|---|
| ISO 3506-1:2020 | Covered corrosion-resistant stainless steel bolts, screws, and studs | Mechanical and physical properties and property classes for covered fasteners | Fastener type, grade, class, dimensions, temperature, and joint environment; the reference does not establish anchor-system performance |
| ISO 10474:2013 | Inspection documents for steel-product deliveries | Inspection-document types supplied according to order requirements | Certificate authenticity, traceability, test validity, and conformity |
| ASTM A967/A967M-25 | Chemical passivation treatments for stainless steel parts | Several passivation treatments and qualitative checks for treatment effectiveness | Grade, treatment, and acceptance criteria remain application-specific and subject to purchaser-supplier agreement |
A stainless designation by itself does not specify a part. The same nominal grade can be supplied in different product forms — bar, forging, casting — each with different inspection and evidence expectations. ISO 3506-1:2020 defines mechanical and physical properties and property classes for covered corrosion-resistant stainless fasteners, which gives the buyer a basis for comparing property classes when the anchor or its threaded elements fall within that standard’s scope. It does not establish how the finished anchor system will perform once installed, so a property-class reference supports the fastener element of the specification without resolving questions about the assembled anchor’s behavior in its installed condition.
Passivation scope is a separate decision from grade selection. ASTM A967/A967M-25 covers several passivation treatments and the qualitative checks used to confirm treatment effectiveness, but it leaves the choice of treatment and the acceptance criteria to agreement between purchaser and supplier. This matters because passivation requirements change with the anchor’s service environment — an anchor in a sheltered interior application does not carry the same passivation expectation as one exposed to washdown, coastal air, or other corrosive conditions, and the specification has to state which condition applies rather than leaving the supplier to infer it from the grade alone.
Inspection documentation closes the material question but does not answer it by itself. ISO 10474:2013 defines the types of inspection documents that can accompany a steel-product delivery according to what the order specifies, but the existence of a named document type does not establish that a particular certificate is authentic, traceable to the actual lot delivered, or backed by valid test results. The buyer’s order has to specify which inspection-document type is required, and the acceptance process has to confirm that the document received actually corresponds to the material received, rather than treating the presence of a certificate as sufficient on its own.
Prototype, inspection, and traceability expectations
A prototype or first-article unit exists to surface the gap between what the drawing describes and what the manufacturing process actually produces. That gap can appear in dimensional conformance, in how a finish behaves across the part’s geometry, or in how a thread engages its mating feature once both parts exist physically rather than on paper. The value of a first article depends on inspecting it against the same criteria that will apply to production lots — if the first-article inspection checks different features or uses a looser method than the production inspection plan, the prototype does not actually validate what the buyer needs validated.
Where a prototype reveals a needed change, the change has to be written back into the controlled drawing and the purchase order before repeat production begins. An unrecorded verbal agreement to adjust a dimension, a finish step, or a tolerance creates a mismatch the moment a second batch is ordered against the original drawing, because nothing in the documentation reflects what was actually agreed after the first article was reviewed.
Lot traceability and inspection records serve the buyer at two different points. During the order, they let the buyer confirm that the material and process used match what the specification required. After installation, they let the buyer trace a specific installed anchor back to its production lot if a question arises about that lot’s conformance. Both uses depend on the inspection method and acceptance record being defined before parts are made — a method decided after the fact cannot be used to validate parts already produced, and an acceptance record without a defined method only documents that an inspection occurred, not what it confirmed.
These expectations connect directly to how a buyer evaluates a supplier’s quality system before placing a custom order, since incoming material checks, in-process inspection, and final inspection each address a different point where nonconformance can enter the part.
Order release controls for revisions and repeat batches
Releasing an order means committing a specific revision of the drawing and its accompanying purchase documents as the basis for production. That commitment only holds value if every subsequent change — whether from a first-article finding, a field fit issue, or a supplier-proposed process adjustment — is captured as a new, identified revision rather than an informal update to the existing one. Where a change is agreed but not reflected in a reissued drawing, the next repeat batch has no documented basis for incorporating it, and the supplier may default back to the last released revision.
This is where the buyer’s own project information carries forward into how a repeat order is quoted and produced. The dimensions, finish requirements, and interface details the buyer supplies at the original specification stage become the reference point a configuration or quotation review returns to for every subsequent batch, which is why keeping that information current in the released documents — not just in correspondence — determines whether a second or third production run matches the first.
Repeat-batch control also depends on distinguishing a true repeat order from a variant. If a later order changes even one interface dimension, a finish requirement, or a mating-part detail, it is not a repeat of the prior revision but a new configuration that needs its own review against the categories already established — drawing and interfaces, material evidence, finish and passivation scope, and inspection and traceability requirements. Treating a modified order as an unchanged repeat risks carrying forward acceptance criteria that no longer match the part actually being produced.
Where project conditions are stable and the mating assembly has not changed, the released revision can carry forward with minimal re-review, since the interfaces and evidence requirements were already settled. Where the project has introduced a new mating component, a different service environment, or a revised finish requirement, the order needs to return to the specification stage before release, because the prior revision no longer describes what the assembly actually requires. 锚固系统 and their adjustable base plate counterparts are typical examples of components whose interface details must be re-confirmed whenever either side of that pairing changes, since a revision to one side without corresponding review of the other reintroduces the coordination risk the original specification was meant to close.
常见问题
问: What should I provide before requesting a custom stainless steel railing anchor quotation?
A: Provide a controlled drawing that identifies the connection interfaces, critical dimensions, threads, tolerances, and mating parts. Also state the service environment and the required material evidence, finish and passivation scope, inspection and traceability records, and protective packaging requirements.
问: Is specifying 304 or 316 stainless steel enough for an OEM or ODM anchor order?
A: No. Define the applicable product form and required evidence, then confirm the fastener type, grade, property class, dimensions, temperature, and joint environment relevant to the project.
问: Does compliance with ISO 3506-1 establish the performance of the complete anchor system?
A: No. The reference addresses mechanical and physical properties and property classes for covered stainless steel bolts, screws, and studs; the complete anchor system still needs project-specific evaluation based on its interfaces, mating parts, dimensions, and joint environment.
问: How should finish and passivation requirements be written into the order?
A: State the required finish and passivation scope, then record the stainless grade, selected treatment, and acceptance criteria agreed for the application. A reference to ASTM A967/A967M alone does not settle those project-specific choices.
问: What must happen after a prototype or first-article change?
A: Incorporate the approved change into the released drawing and purchase documents before repeat production. Confirm that the repeat order identifies the same released revision so purchasing, production, and inspection work from one controlled basis.
问: Does an ISO 10474 inspection document prove traceability and conformity by itself?
A: No. Specify the required inspection-document type, but separately verify document authenticity, lot traceability, test validity, and conformity to the agreed order requirements.