A railing anchor that passes inspection on the surface can still conceal a drilling error, a skipped cleaning pass, or a cure that never reached its design strength. Once the base plate or cover is set, the evidence for that judgment disappears, which means the controls that protect the anchor have to be applied and recorded while the work is still visible, not reconstructed afterward.
What each installation control protects against
Each stage of anchor installation exists to prevent a distinct failure mode, and treating them as one combined “installation step” is where the protection breaks down. Drilling establishes the hole geometry the anchor system depends on; if the hole is oversized, undersized, misaligned, or cut into an unsuitable substrate condition, no later step corrects it. Hole cleaning removes drilling residue that would otherwise interfere with adhesive bond or mechanical expansion; a hole that looks finished can still carry dust or debris that the anchor system’s instructions were written to exclude. Anchor insertion and cure, for adhesive systems, establish the chemical bond strength over a defined time and condition; this is a process that continues after the installer has moved to the next post and is not visible once complete. Torque application for mechanical fasteners is a separate action still, intended to seat the fastener per a specified procedure, and it happens after the anchor is already in place.
The reason these cannot be collapsed into a single pass/fail check is that a later step can visually mask an earlier one. A properly torqued bolt looks identical whether the hole beneath it was cleaned correctly or not. A cured adhesive anchor looks identical whether it was loaded before or after its approved cure period. This is why the controls need to be understood as protecting against different causes: hole condition protects against poor substrate engagement, cleaning protects against bond or expansion interference, cure state protects against premature loading, and torque procedure protects against inconsistent fastener seating. Where a project treats these as one combined sign-off, the specific cause of a later problem becomes difficult to isolate, because the record does not distinguish which control was actually satisfied and which was assumed.
Drilling and hole-cleaning steps tied to the selected system
Drilling and hole-cleaning requirements are not general practices that apply the same way across anchor types; they are instructions written for the exact anchor system selected for the project, and they only apply when the installation matches the conditions those instructions cover. The applicability rule has four conditions that need to be checked together: the anchor system, the actual hole condition achieved, the substrate the anchor is set into, and the service temperature the installation will experience. If any one of these differs from what the selected system’s instructions assume, the drilling and cleaning steps written for that system may not transfer to the actual job.
This matters because hole condition and substrate interact directly with how an anchor develops its holding capacity. A hole drilled to the correct diameter in one substrate type does not necessarily behave the same way in another; the same nominal hole size can leave different amounts of residual dust, different wall roughness, or different moisture retention depending on what the hole was cut into. Service temperature changes the behavior of adhesive products and the clearances assumed for mechanical anchors, so an installation expected to operate in one temperature range cannot assume that instructions written for a different range still apply.
Where the actual job conditions match what the selected system’s instructions were written for, the drilling and cleaning steps can be followed as documented. Where any condition differs, the project team needs to return to the anchor system’s own instructions rather than substitute a generic drilling or cleaning routine, because the selected system instructions are the only source that ties hole preparation to the anchor’s expected performance. ESANG’s Sistemas de ancoragem are supplied to match the installation conditions a buyer specifies, which is why confirming hole condition, substrate, and service temperature against the selected anchor’s instructions needs to happen before drilling begins, not after.
Adhesive cure conditions and permitted loading point
| Record item | What to capture | Uso da decisão |
|---|---|---|
| Anchor identification | Exact adhesive anchor product and batch | Connects the installation record to the selected anchor system |
| Procedure applicability | Hole condition, substrate, and service temperature covered by the selected system instructions | Checks whether the instructions apply to the actual installation conditions |
| Prazo de instalação | Installation time | Provides the time record needed to evaluate cure state under the approved procedure |
| Loading release | Permitted loading point defined by the approved procedure | Identifies when loading may begin; a generic cure value is not a substitute |
Adhesive anchors gain their holding capacity through a chemical cure process that develops over time under conditions the manufacturer’s approved procedure defines. The point at which the anchor may be loaded is not a fixed duration that applies across products; it is a release point the approved procedure sets based on the product formulation, the installation temperature, and the substrate. Treating cure as “enough time has passed” substitutes a general assumption for the specific release condition the procedure defines, and the two do not necessarily agree.
Because cure state cannot be inspected visually once the anchor is set, the installation record has to substitute for direct observation. Capturing which adhesive product and batch was used ties the installation to the correct set of instructions, since cure behavior is specific to the product. Recording the installation time establishes the reference point the cure duration is measured from; without it, there is no way to determine whether the permitted loading point has actually been reached. The loading release itself then comes from the approved procedure’s defined point, not from a generic cure value assumed to apply across adhesive products or temperature conditions.
This sequence matters most where project schedules create pressure to load a railing anchor soon after installation. If the installation record does not include product identity, batch, and installation time, there is no basis for confirming that the structure has reached its approved loading point at the time the railing is actually loaded, whether that loading comes from installation of the railing itself or from in-service use. The approved procedure defined for the specific adhesive anchor product is the only source that establishes when loading may begin; a cure time assumed from a different product or a different installation temperature does not substitute for it.
Torque application records for mechanical fasteners
Mechanical fasteners rely on torque application to develop clamp force, and recording that torque was applied according to a defined procedure documents that the installation step occurred. What a torque record does not establish is the resulting clamp force itself. ISO 3506-1 defines mechanical and physical properties for corrosion-resistant stainless steel fasteners covered by that standard, including bolts, screws, and studs, but it does not define torque-clamp-force relationships. This means a torque value recorded during installation confirms that a torque procedure was executed; it does not, on its own, confirm the clamp force that resulted from that application.
The distinction matters because torque and clamp force are related through factors that vary by joint condition, including friction at the fastener interface and the condition of the mating surfaces. The same applied torque can produce different clamp force outcomes depending on these joint-specific factors, which is why a torque record should be understood as evidence that the procedure was followed, not as a direct measurement of the structural outcome the clamp force is meant to achieve. Where a project needs to confirm actual clamp force rather than procedure execution, that confirmation requires a different kind of verification than a torque record alone provides.
This boundary affects how the torque record should be used in practice. If the project documentation treats a torque record as proof of adequate clamp force, it is asserting something the record does not support. If instead the torque record is understood as documentation that the defined torque procedure was carried out, the fastener scope, grade, class, dimensions, and joint environment still need to be verified separately against the fastener’s specification, since clamp force and torque cannot be inferred from each other without that separate verification. The buyer or installer should confirm which claim the project’s documentation actually intends the torque record to support before relying on it for structural sign-off.
Inspection hold points before railing installation hides the work
| Hold point | Check or record before continuing | Control boundary |
|---|---|---|
| After drilling | Drilled holes and actual hole condition against the selected system instructions | Retains a witness point before the railing base hides the holes |
| After hole cleaning | Completion of the cleaning step required by the selected system instructions | Keeps cleaning separate because a completed fastener can conceal a missed step |
| At adhesive anchor insertion | Product, batch, and installation time | Preserves the records needed to determine cure state and the approved loading point |
| Before loading an adhesive anchor | Cure state and permitted loading point from the approved procedure | Loading release depends on the approved procedure, not a generic cure value |
| After torque application to a mechanical fastener | Torque procedure execution record | Documents procedure execution but does not establish clamp force under ISO 3506-1 |
| Before the railing base hides the work | Anchor markings and drilled-hole evidence needed for inspection | Preserves evidence that may no longer be visible after installation |
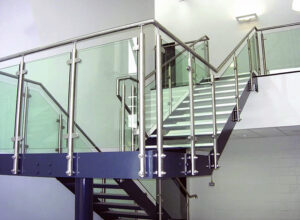
The anchor installation stages described above, drilling, cleaning, adhesive insertion and cure, and torque application, share one practical constraint: each becomes invisible once the next construction stage covers it. A railing base plate, once set, hides the drilled hole condition beneath it. A cured adhesive anchor, once loaded and in service, no longer shows whether it was loaded before or after its approved cure point. A torqued fastener shows the same finished appearance whether the hole beneath it was properly cleaned or not. This is the reason these stages need to be treated as separate witness or record points rather than a single final inspection.
The practical consequence is that inspection planning has to happen before the work begins, not after the railing base is in place. Once base plates or covers conceal the anchor markings and the drilled holes, evidence that would let a later reviewer confirm what was actually done is no longer available to observe directly; only the records created during installation remain. This is consistent with the evidence structure described in related guidance on railing post inspection evidence, where anchor condition, weld condition, and base plate alignment all depend on records made while the work was still visible, and with the mounting mistakes that follow when anchor and substrate conditions are not confirmed at the time of installation rather than afterward.
ASTM E894-88 (2004) identifies railing anchorage, anchor tension and shear, post-base testing, and mounting verification as relevant subjects for permanent metal railing systems, though the installation requirements and acceptance values for a specific project still depend on the selected anchor system’s own documents and the project design, not on the standard’s metadata alone. Where a project buyer is coordinating with ESANG on anchor selection, the installation conditions, substrate, and service temperature supplied at that stage inform which anchoring system is configured for the order, which is a separate question from how the installation itself is witnessed and recorded on site. Planning the hold points for drilling, cleaning, adhesive insertion, cure release, and torque application before the railing base is set is what preserves the ability to confirm, after the fact, that each stage was actually completed as the selected system’s instructions required.
Perguntas frequentes
P: Can one installation checklist cover both adhesive and mechanical railing anchors?
A: It can use the same staged hold-point structure, but the required records must reflect the anchor type. Adhesive anchors need product, batch, installation-time, cure-state, and loading-release records, while a mechanical-fastener torque record documents procedure execution without establishing clamp force.
P: What must be confirmed before using drilling, cleaning, torque, or cure instructions on site?
A: Confirm that the instructions apply to the exact anchor system, actual hole condition, substrate, and service temperature. If any of those conditions fall outside the selected system instructions, a generic torque or cure value is not a valid substitute.
P: What should be planned before anchor work begins so later inspection remains possible?
A: Set witness points for the drilled holes, required cleaning step, anchor identification, and installation records before the railing base can hide them. The work sequence should make each hold point available for its required check before the next stage proceeds.
P: When can an adhesive railing anchor be released for loading?
A: Release it only at the permitted loading point defined by the approved procedure for the actual installation conditions. Use the recorded product and batch, installation time, and cure state to make that decision rather than applying a generic cure duration.
P: Does a torque record prove that a mechanical fastener achieved the required clamp force?
A: No. It can show that the specified torque procedure was carried out, but ISO 3506-1 does not establish torque-to-clamp-force properties; the project must use the selected anchor system’s applicable procedure and acceptance basis for that decision.